


Solid carbide ball nose end mill, short, twin blade
CTR-RADI-WN-AL-SC-W-D6,0MM
Art.-no. 5443301258
EAN 4055375917237


Register now and access more than 125,000 products
Datasheets(X)

 | |
Product code | 6925 |
Material to be processed | Aluminium, Copper, Brass, Plastic |
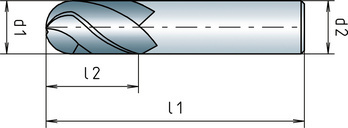
Diameter (d1) | 6 mm |
Shank diameter (d2) | 6 mm |
Standards | CS |
Construction length | Short |
Shank style | Cylindrical |
Cutting material | SC |
Surface | Plain |
Coolant supply | External |
Twist angle | 30° |
Length (l1) | 50 mm |
Chip flute length (l2) | 16 mm |
Number of cutting edges (Z) | 2 PCS |
Tolerance of cutting edge diameter | h10 |
Tolerance of shank diameter | h6 |
Material of sub-group | Aluminium, Copper, Brass, Plastics |
| Legend | ||
| E = emulsion |  | ae = 0.05xd1 |
| vc = cutting speed [m/min] | ||
| fz = feed per tooth [mm/t] | ap = 0.05xd1 | |
| ae = cutting thickness (radial) | ||
| ap = cutting thickness (axial) | ||
| The suggested cutting values are reference values and must be adapted to the respective conditions. | ||
| Cutting values for roughing copy | ||||||
| For dia. 6-12 | ||||||
| Material designation | Tensile strength | Cooling | vc | fz | ||
| Dia. 6-7.9 | Dia. 8-9.9 | Dia. 10-12 | ||||
| Aluminium, aluminium alloys | < 530 N/mm² | E | 230 | 0,034 | 0,045 | 0,056 |
| Aluminium, cast aluminium alloys < 10 % Si | < 600 N/mm² | E | 180 | 0,034 | 0,045 | 0,056 |
| Aluminium, cast aluminium alloys > 10 % Si | < 600 N/mm² | - | 160 | 0,034 | 0,045 | 0,056 |
| Magnesium, magnesium alloys | < 280 N/mm² | - | 160 | 0,034 | 0,045 | 0,056 |
| Copper, low-alloy | < 350 N/mm² | - | 160 | 0,034 | 0,045 | 0,056 |
| Brass, short-chipping | < 600 N/mm² | - | 140 | 0,034 | 0,045 | 0,056 |
| Brass, long-chipping | < 600 N/mm² | E | 140 | 0,034 | 0,045 | 0,056 |
| Bronze, short-chipping | < 600 N/mm² | E | 110 | 0,034 | 0,045 | 0,056 |
| 650-850 N/mm² | - | 80 | 0,034 | 0,045 | 0,056 | |
| Bronze, long-chipping | < 850 N/mm² | - | 140 | 0,034 | 0,045 | 0,056 |
| 850-1200 N/mm² | - | 110 | 0,034 | 0,045 | 0,056 | |
| Cutting values for roughing copy | ||||||
| For dia. 1-5.9 | ||||||
| Material designation | Tensile strength | Cooling | vc | fz | ||
| Dia. 1-1.9 | Dia. 2-3.9 | Dia. 4-5.9 | ||||
| Aluminium, aluminium alloys | < 530 N/mm² | E | 230 | 0,006 | 0,011 | 0,023 |
| Aluminium, cast aluminium alloys < 10 % Si | < 600 N/mm² | E | 180 | 0,006 | 0,011 | 0,023 |
| Aluminium, cast aluminium alloys > 10 % Si | < 600 N/mm² | - | 160 | 0,006 | 0,011 | 0,023 |
| Magnesium, magnesium alloys | < 280 N/mm² | - | 160 | 0,006 | 0,011 | 0,023 |
| Copper, low-alloy | < 350 N/mm² | - | 160 | 0,006 | 0,011 | 0,023 |
| Brass, short-chipping | < 600 N/mm² | - | 140 | 0,006 | 0,011 | 0,023 |
| Brass, long-chipping | < 600 N/mm² | E | 140 | 0,006 | 0,011 | 0,023 |
| Bronze, short-chipping | < 600 N/mm² | E | 110 | 0,006 | 0,011 | 0,023 |
| 650-850 N/mm² | - | 80 | 0,006 | 0,011 | 0,023 | |
| Bronze, long-chipping | < 850 N/mm² | - | 140 | 0,006 | 0,011 | 0,023 |
| 850-1200 N/mm² | - | 110 | 0,006 | 0,011 | 0,023 | |
| Legend | ||
| E = emulsion | | ae = 0.03xd1 |
| vc = cutting speed [m/min] | ||
| fz = feed per tooth [mm/t] | ap = 0.03xd1 | |
| ae = cutting thickness (radial) | ||
| ap = cutting thickness (axial) | ||
| The suggested cutting values are reference values and must be adapted to the respective conditions. | ||
| Cutting values for finishing copying | ||||||
| For dia. 6-12 | ||||||
| Material designation | Tensile strength | Cooling | vc | fz | ||
| Dia. 6-7.9 | Dia. 8-9.9 | Dia. 10-12 | ||||
| Aluminium, aluminium alloys | < 530 N/mm² | E | 400 | 0,035 | 0,053 | 0,071 |
| Aluminium, cast aluminium alloys < 10 % Si | < 600 N/mm² | E | 300 | 0,035 | 0,053 | 0,071 |
| Aluminium, cast aluminium alloys > 10 % Si | < 600 N/mm² | E | 250 | 0,035 | 0,053 | 0,071 |
| Magnesium, magnesium alloys | < 280 N/mm² | E | 400 | 0,035 | 0,053 | 0,071 |
| Copper, low-alloy | < 350 N/mm² | E | 200 | 0,035 | 0,053 | 0,071 |
| Brass, short-chipping | < 600 N/mm² | - | 180 | 0,035 | 0,053 | 0,071 |
| Brass, long-chipping | < 600 N/mm² | - | 180 | 0,035 | 0,053 | 0,071 |
| Bronze, short-chipping | < 600 N/mm² | - | 180 | 0,035 | 0,053 | 0,071 |
| 650-850 N/mm² | - | 150 | 0,035 | 0,053 | 0,071 | |
| Bronze, long-chipping | < 850 N/mm² | E | 150 | 0,035 | 0,053 | 0,071 |
| 850-1200 N/mm² | E | 120 | 0,035 | 0,053 | 0,071 | |
| Cutting values for finishing copying | ||||||
| For dia. 1-5.9 | ||||||
| Material designation | Tensile strength | Cooling | vc | fz | ||
| Dia. 1-1.9 | Dia. 2-3.9 | Dia. 4-5.9 | ||||
| Aluminium, aluminium alloys | < 530 N/mm² | E | 400 | 0,007 | 0,013 | 0,026 |
| Aluminium, cast aluminium alloys < 10 % Si | < 600 N/mm² | E | 300 | 0,007 | 0,013 | 0,026 |
| Aluminium, cast aluminium alloys > 10 % Si | < 600 N/mm² | E | 250 | 0,007 | 0,013 | 0,026 |
| Magnesium, magnesium alloys | < 280 N/mm² | E | 400 | 0,007 | 0,013 | 0,026 |
| Copper, low-alloy | < 350 N/mm² | E | 200 | 0,007 | 0,013 | 0,026 |
| Brass, short-chipping | < 600 N/mm² | - | 180 | 0,007 | 0,013 | 0,026 |
| Brass, long-chipping | < 600 N/mm² | - | 180 | 0,007 | 0,013 | 0,026 |
| Bronze, short-chipping | < 600 N/mm² | - | 180 | 0,007 | 0,013 | 0,026 |
| 650-850 N/mm² | - | 150 | 0,007 | 0,013 | 0,026 | |
| Bronze, long-chipping | < 850 N/mm² | E | 150 | 0,007 | 0,013 | 0,026 |
| 850-1200 N/mm² | E | 120 | 0,007 | 0,013 | 0,026 | |
Last viewed

Bitumen tape with aluminium lamination

Socket Head Cap Screw With hexagon socket

GEFU® thread-rolling screw with Taptite 2000® thread, flattened half round head with collar and hexalobular drive

XZN bit for door wrenches

Replacement hose for tyre inflator

Hexagon nut

Hexagonal bolt with shank ISO 4014, steel 8.8, plain

Key, high profile DIN 6885, steel, plain, shape AB

Hex head screw with thread up to head ISO 4017, A2-70 stainless steel, plain

Round head screw with slot and nut W-0231, steel 04.8, zinc-plated with nut, slotted