


Solid carbide cutter SPEEDCUT Ultra HRC XL HA
CTR-SC-SP-WNXL-HS-EL-TNS-HA-D16,0MM
Art.-no. 5443300880
EAN 4055375919736


Register now and access more than 125,000 products
Datasheets(X)

 | |
Product code | 7287 |
Material to be processed | Cast metal, Hard and tough material |
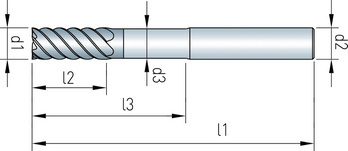
Diameter (d1) | 16 mm |
Shank diameter (d2) | 16 mm |
Standards | CS |
Construction length | Extra long |
Shank style | Cylindrical DIN 6535-HA |
Cutting material | SC |
Surface | TiAlN-S |
Coolant supply | External |
Twist angle | 50° |
Length (l1) | 105 mm |
Cutting edge length (l2) | 50 mm |
Number of cutting edges (Z) | 8 PCS |
Corner chamfer | 0.10 mm |
Tolerance of cutting edge diameter | e8 |
Tolerance of shank diameter | h5 |
Material of sub-group | Alloyed tempering steels < 1000 N/mm², Nitriding steels < 1300 N/mm², Grey cast iron, Malleable cast iron, Steels > 45 HRC |
| Cutting values for finishing contour | ||||||
| For dia. 12 - dia. 20 | ||||||
| Material designation | Tensile strength | Cooling | vc | fz | ||
| Dia. 12 | Dia. 16 | Dia. 20 | ||||
| General structural steels | < 500 N/mm² | L + E | 330 | 0,065 | 0,080 | 0,100 |
| 500–850 N/mm² | L + E | 260 | 0,065 | 0,075 | 0,090 | |
| Machining steels | < 850 N/mm² | L + E | 260 | 0,060 | 0,075 | 0,090 |
| 850–1000 N/mm² | L + E | 255 | 0,050 | 0,065 | 0,080 | |
| Non-alloyed tempering steels | < 700 N/mm² | L + E | 290 | 0,065 | 0,075 | 0,090 |
| 700–850 N/mm² | L + E | 260 | 0,060 | 0,075 | 0,090 | |
| 850–1000 N/mm² | L + E | 255 | 0,050 | 0,065 | 0,080 | |
| Alloyed tempering steels | 850–1000 N/mm² | L + E | 240 | 0,050 | 0,065 | 0,080 |
| 1000–1200 N/mm² | L + E | 210 | 0,050 | 0,060 | 0,075 | |
| Non-alloyed case-hardening steels | < 750 N/mm² | L + E | 330 | 0,065 | 0,080 | 0,100 |
| Alloyed case-hardening steels | < 1000 N/mm² | L + E | 255 | 0,050 | 0,065 | 0,080 |
| 1000–1200 N/mm² | L + E | 210 | 0,050 | 0,060 | 0,075 | |
| Nitriding steels | < 1000 N/mm² | L + E | 255 | 0,050 | 0,065 | 0,080 |
| 1000–1200 N/mm² | L + E | 210 | 0,050 | 0,060 | 0,075 | |
| Tool steels | < 850 N/mm² | L + E | 265 | 0,050 | 0,065 | 0,080 |
| 850–1100 N/mm² | L + E | 255 | 0,050 | 0,060 | 0,075 | |
| High-speed steels | 850–1200 N/mm² | L + E | 145 | 0,050 | 0,060 | 0,075 |
| Spring steels | < 1200 N/mm² | L + E | 145 | 0,050 | 0,060 | 0,075 |
| Stainless steels, sulphurated | < 700 N/mm² | E | 175 | 0,055 | 0,065 | 0,080 |
| Stainless steels, austenitic | < 700 N/mm² | E | 155 | 0,050 | 0,060 | 0,075 |
| < 850 N/mm² | E | 145 | 0,050 | 0,060 | 0,075 | |
| Stainless steels, martensitic | < 1100 N/mm² | E | 130 | 0,050 | 0,060 | 0,075 |
| Special alloys | < 1200 N/mm² | E | 100 | 0,045 | 0,055 | 0,065 |
| Titanium, titanium alloys | < 850 N/mm² | E | 100 | 0,050 | 0,060 | 0,075 |
| Cast iron | < 180 HB | - | 225 | 0,080 | 0,095 | 0,115 |
| < 180 HB | - | 145 | 0,075 | 0,090 | 0,110 | |
| Spheroidal graphite, malleable iron | < 180 HB | - | 175 | 0,080 | 0,095 | 0,115 |
| > 260 HB | E | 145 | 0,075 | 0,090 | 0,110 | |
| Legend | ||
| T= dry | 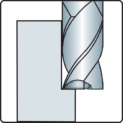 | ae = 0.02xd1 |
| vc = cutting speed [m/min] | ||
| fz = feed per tooth [mm/z] | ap = 1.5xd1 | |
| ae = cutting thickness (radial) | ||
| ap = cutting thickness (axial) | ||
| The cutting speeds listed refer to all tool types according to DIN 6527K or DIN6527L. For XL Series end mills, it is recommended to reduce the cutting speed by 30%. | ||
Last viewed

WÜRTH MODYF STAR COTTON bib overalls

T-handle 2C hex key with ball head with side drive

Snap ring shape SW for shaft Type SW, steel plain

Hex head screw with thread up to head ISO 4017, A2-70 stainless steel, plain
Snap ring shape SW for shaft Type SW, steel plain
Snap ring shape SW for shaft Type SW, steel plain

SHARK Pro plastic multi-purpose anchor assortment 620 pieces

Electric strike, type SA
Air cndtnng. srvc. unit, vhcls., accss.

FLEXEN Plus S3 rubber foam refrigeration insulation Continuous panels