


Solid carbide end mill, short, twin blade
ENDMIL-WN-ALU-SC-W-D16
Art.-no. 5443301723
EAN 4055375917138


Register now and access more than 125,000 products
Datasheets(X)

 | |
Product code | 6915 |
Material to be processed | Aluminium, Copper, Brass, Plastic |
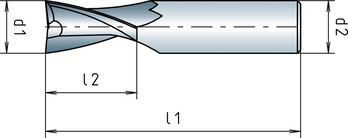
Diameter (d1) | 16 mm |
Shank diameter (d2) | 16 mm |
Standards | CS |
Construction length | Short |
Shank style | Cylindrical |
Cutting material | SC |
Surface | Plain |
Coolant supply | External |
Twist angle | 30° |
Length (l1) | 82 mm |
Cutting edge length (l2) | 28 mm |
Number of cutting edges (Z) | 2 PCS |
Tolerance of cutting edge diameter | h10 |
Tolerance of shank diameter | h6 |
Material of sub-group | Aluminium, Copper, Brass, Plastics |
| Legend | ||
| E = emulsion | 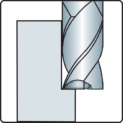 | ae = 0.1xd1 |
| vc = cutting speed [m/min] | ||
| fz = feed per tooth [mm/t] | ap = 1.5xd1 | |
| ae = cutting thickness (radial) | ||
| ap = cutting thickness (axial) | ||
| The suggested cutting values are reference values and must be adapted to the respective conditions. | ||
| Cutting values for finishing contour | |||||||
| For dia. 10-20 | |||||||
| Material designation | Tensile strength | Cooling | vc | fz | |||
| Dia. 10-11.9 | Dia. 12-15.9 | Dia. 16-19.9 | Dia. 20 | ||||
| Aluminium, aluminium alloys | < 530 N/mm² | E | 400 | 0,063 | 0,079 | 0,101 | 0,126 |
| Aluminium, cast aluminium alloys < 10 % Si | < 600 N/mm² | E | 300 | 0,063 | 0,079 | 0,101 | 0,126 |
| Aluminium, cast aluminium alloys > 10 % Si | < 600 N/mm131 | E | 250 | 0,063 | 0,079 | 0,101 | 0,126 |
| Magnesium, magnesium alloys | < 280 N/mm² | E | 400 | 0,063 | 0,079 | 0,101 | 0,126 |
| Copper, low-alloy | < 350 N/mm² | E | 200 | 0,063 | 0,079 | 0,101 | 0,126 |
| Brass, short-chipping | < 600 N/mm² | - | 180 | 0,063 | 0,079 | 0,101 | 0,126 |
| Brass, long-chipping | < 600 N/mm² | - | 180 | 0,063 | 0,079 | 0,101 | 0,126 |
| Bronze, short-chipping | < 600 N/mm² | - | 180 | 0,063 | 0,079 | 0,101 | 0,126 |
| 650-850 N/mm² | - | 150 | 0,063 | 0,079 | 0,101 | 0,126 | |
| Bronze, long-chipping | < 850 N/mm² | E | 150 | 0,063 | 0,079 | 0,101 | 0,126 |
| 850-1200 N/mm² | E | 120 | 0,063 | 0,079 | 0,101 | 0,126 | |
| Graphite | - | 90 | 0,072 | 0,089 | 0,107 | 0,125 | |
| Cutting values for finishing contour | ||||||||
| For dia. 1-9.9 | ||||||||
| Material designation | Tensile strength | Cooling | vc | fz | ||||
| Dia. 1-1.9 | Dia. 2-3.9 | Dia. 4-5.9 | Dia. 6-7.9 | Dia. 8-9.9 | ||||
| Aluminium, aluminium alloys | < 530 N/mm² | E | 400 | 0,006 | 0,012 | 0,024 | 0,031 | 0,047 |
| Aluminium, cast aluminium alloys < 10 % Si | < 600 N/mm² | E | 300 | 0,006 | 0,012 | 0,024 | 0,031 | 0,047 |
| Aluminium, cast aluminium alloys > 10 % Si | < 600 N/mm² | E | 250 | 0,006 | 0,012 | 0,024 | 0,031 | 0,047 |
| Magnesium, magnesium alloys | < 280 N/mm² | E | 400 | 0,006 | 0,012 | 0,024 | 0,031 | 0,047 |
| Copper, low-alloy | < 350 N/mm² | E | 200 | 0,006 | 0,012 | 0,024 | 0,031 | 0,047 |
| Brass, short-chipping | < 600 N/mm² | - | 180 | 0,006 | 0,012 | 0,024 | 0,031 | 0,047 |
| Brass, long-chipping | < 600 N/mm² | - | 180 | 0,006 | 0,012 | 0,024 | 0,031 | 0,047 |
| Bronze, short-chipping | < 600 N/mm² | - | 180 | 0,006 | 0,012 | 0,024 | 0,031 | 0,047 |
| 650-850 N/mm² | - | 150 | 0,006 | 0,012 | 0,024 | 0,031 | 0,047 | |
| Bronze, long-chipping | < 850 N/mm² | E | 150 | 0,006 | 0,012 | 0,024 | 0,031 | 0,047 |
| 850-1200 N/mm² | E | 120 | 0,006 | 0,012 | 0,024 | 0,031 | 0,047 | |
| Graphite | - | 90 | 0,007 | 0,014 | 0,020 | 0,027 | 0,054 | |
| Legend | ||
| E = emulsion | | ae = 0.5xd1 |
| vc = cutting speed [m/min] | ||
| fz = feed per tooth [mm/t] | ap = 1xd1 | |
| ae = cutting thickness (radial) | ||
| ap = cutting thickness (axial) | ||
| The suggested cutting values are reference values and must be adapted to the respective conditions. | ||
| Cutting values for roughing contour | |||||||
| For dia. 10-20 | |||||||
| Material designation | Tensile strength | Cooling | vc | fz | |||
| Dia. 10-11.9 | Dia. 12-15.9 | Dia. 16-19.9 | Dia. 20 | ||||
| Aluminium, aluminium alloys | < 530 N/mm² | E | 200 | 0,050 | 0,070 | 0,090 | 0,120 |
| Aluminium, cast aluminium alloys < 10 % Si | < 600 N/mm² | E | 150 | 0,050 | 0,070 | 0,090 | 0,120 |
| Aluminium, cast aluminium alloys > 10 % Si | < 600 N/mm131 | E | 120 | 0,050 | 0,070 | 0,090 | 0,120 |
| Magnesium, magnesium alloys | < 280 N/mm² | E | 200 | 0,050 | 0,070 | 0,090 | 0,120 |
| Copper, low-alloy | < 350 N/mm² | E | 150 | 0,050 | 0,070 | 0,090 | 0,120 |
| Brass, short-chipping | < 600 N/mm² | - | 140 | 0,050 | 0,070 | 0,090 | 0,120 |
| Brass, long-chipping | < 600 N/mm² | - | 140 | 0,050 | 0,070 | 0,090 | 0,120 |
| Bronze, short-chipping | < 600 N/mm² | - | 140 | 0,050 | 0,070 | 0,090 | 0,120 |
| 650-850 N/mm² | - | 120 | 0,050 | 0,070 | 0,090 | 0,120 | |
| Bronze, long-chipping | < 850 N/mm² | E | 120 | 0,050 | 0,070 | 0,090 | 0,120 |
| 850-1200 N/mm² | E | 95 | 0,050 | 0,070 | 0,090 | 0,120 | |
| Graphite | - | 70 | 0,050 | 0,060 | 0,080 | 0,100 | |
| Cutting values for roughing contour | ||||||||
| For dia. 1-9.9 | ||||||||
| Material designation | Tensile strength | Cooling | vc | fz | ||||
| Dia. 1-1.9 | Dia. 2-3.9 | Dia. 4-5.9 | Dia. 6-7.9 | Dia. 8-9.9 | ||||
| Aluminium, aluminium alloys | < 530 N/mm² | E | 200 | 0,005 | 0,010 | 0,020 | 0,030 | 0,040 |
| Aluminium, cast aluminium alloys < 10 % Si | < 600 N/mm² | E | 150 | 0,005 | 0,010 | 0,020 | 0,030 | 0,040 |
| Aluminium, cast aluminium alloys > 10 % Si | < 600 N/mm131 | E | 120 | 0,005 | 0,010 | 0,020 | 0,030 | 0,040 |
| Magnesium, magnesium alloys | < 280 N/mm² | E | 200 | 0,005 | 0,010 | 0,020 | 0,030 | 0,040 |
| Copper, low-alloy | < 350 N/mm² | E | 150 | 0,005 | 0,010 | 0,020 | 0,030 | 0,040 |
| Brass, short-chipping | < 600 N/mm² | - | 140 | 0,005 | 0,010 | 0,020 | 0,030 | 0,040 |
| Brass, long-chipping | < 600 N/mm² | - | 140 | 0,005 | 0,010 | 0,020 | 0,030 | 0,040 |
| Bronze, short-chipping | < 600 N/mm² | - | 140 | 0,005 | 0,010 | 0,020 | 0,030 | 0,040 |
| 650-850 N/mm² | - | 120 | 0,005 | 0,010 | 0,020 | 0,030 | 0,040 | |
| Bronze, long-chipping | < 850 N/mm² | E | 120 | 0,005 | 0,010 | 0,020 | 0,030 | 0,040 |
| 850-1200 N/mm² | E | 95 | 0,005 | 0,010 | 0,020 | 0,030 | 0,040 | |
| Graphite | - | 70 | 0,005 | 0,010 | 0,020 | 0,030 | 0,040 | |
Last viewed

ERGOPOWER PAD wireless charging pad

Hexagonal bolt with half dog point and small hexagon DIN 564, plain A2 stainless steel

Support clip Nova Grip steel C45, hot-dip galvanised

VARIFIX Systemfix 41 channel nut With threaded rod

Hexalobular-type cheese head screw, low head

Aluminium rail connector

Fuel hose clip Power with high tightening torque

Scaffolding anchor system

Solution 392 furniture castor set without locking device

ASSY® 4 CSMP ZiNi timber screw Steel zinc-nickel partial thread countersunk milling pocket head