


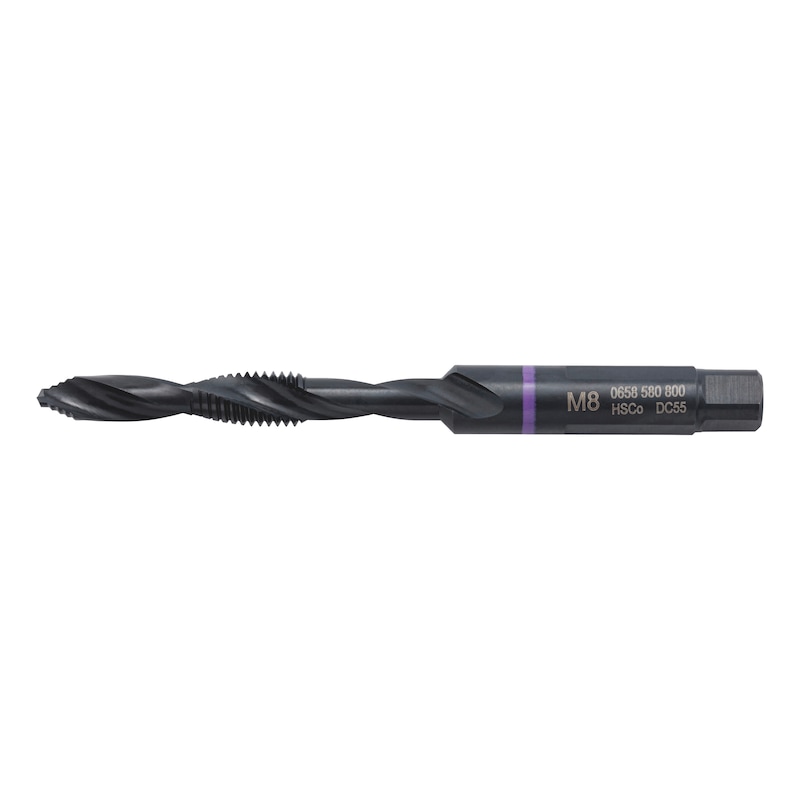
Combination screw tap assortment HSCo SMART STEP 6 pieces
MATAP-SET-KOMBI-HSCO-SMARTSTEP-(M3-M10)
Art.-no. 0658580006
EAN 4065746562300


Register now and access more than 125,000 products
Save time and work easily
- 3-in-1 function for drilling, thread cutting and countersinking/deburring in just 1 operation.
- No tool change required. This saves processing time and reduces the amount of work.
- SMART STEP technology for up to 100 % faster work compared to conventional combination screw taps.
- Gentle drilling due to optimised cutting edge geometry.
Precise results
- Optimal centring even on curved surfaces.
- High-precision, circular holes provide a reliable foundation for subsequent thread cutting.
- Through hole thread true to gauge according to ISO 2 (6H).
Versatile and durable
- Suitable for processing sheet metal and thicker workpieces.
- Enables bore holes, threads and countersinking or deburring up to twice as deep as conventional combination screw taps: 2 x D instead of 1 x D.
- Suitable for nearly all materials.
- SMART STEP technology and HSCo cutting material increase service life compared to conventional combination screw taps.
Practical design and packaging
- The newly developed shank generation with a combination of 3-flat and straight shank with square drive ensures optimum power transmission.
- The 3-flat shank prevents spinning in the drill chuck and protects it from damage.
- Compact and practical system box suitable for the ORSY system with useful features such as stackability, optimised joint and simple opening
- Product packaging made from 100 % PCR (recycled plastic from household waste).
- Available exclusively from WÜRTH.
- Only suitable for through hole threads.
- Countersinks in accordance with DIN 74-1 for countersunk head screws (in accordance with DIN 7991) are not possible.
- For use in cordless drill drivers as well as on hand-held, pillar and upright drills.
- Sufficient coolant and lubricant must be added.
Datasheets(X)

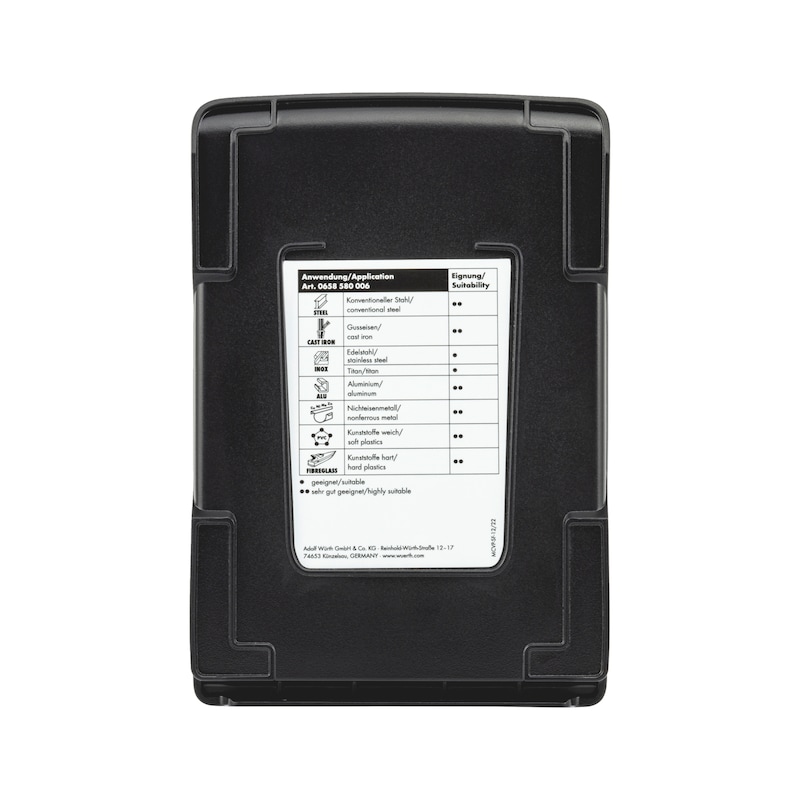
- Suitable for through holes in non-ferrous metals, such as aluminium and brass, plus plastics with a material thickness of up to 2xD. For both hand-held and stationary use.
- Suitable for machining steel materials up to 1,000 N/mm² and cast metal with a material thickness of up to 2xD in stationary use; for material thicknesses of up to 1.5xD in hand-held use.
- Suitable for machining stainless steels and titanium with a material thickness of up to 1xD in stationary use.
- After the drilling process, it is essential to significantly reduce the rotation speed for thread cutting and countersinking/deburring.
- Sufficient coolant and lubricant must be used.
- Be sure to work in a straight line. Avoid tilting at all costs: Risk of tool breakage!
- Before reversing the combination screw tap, make sure to remove all threads of the tool from the drill hole. Failure to do so may cause cutting edges to chip or the tool to break.
Number of pieces in assortment/set | 6 PCS |
Material to be processed | Steel, Cast metal, Stainless steel, Titanium, Non-ferrous metal |
Quality | ZEBRA-Premium |
Hole type | Clearance hole ≤ 2xD |
Cutting material | HSCo |
Surface | Vaporised |
Suitable for machine type | Cordless screwdrivers, Drill, Pedestal drilling machine |
Suitable for tensile strength up to | 1200 N/mm² |
Thread type | Metric thread |
Service life (points system) | 4 of 4 points |
Trueness to gauge (points system) | 4 of 4 points |
Versatility (points system) | 4 of 4 points |
Cutting behaviour (points system) | 4 of 4 points |
Chip formation (points system) | 4 of 4 points |
Material of sub-group | General structural steels, Non-alloyed tempering steels, Alloyed tempering steels, Nitriding steels, Tool steels, High-speed steels, Cast iron, Ductile iron, Malleable cast iron, White cast iron, Stainless steels, sulphurated, Stainless steels, austenitic, Stainless steels, martensitic, Titanium, Titanium alloys, Spring steels, Aluminium, Aluminium alloys, Aluminium casting alloys (<10% silicon), Aluminium wrought alloys, Plastics, thermoset, Plastics, thermoplastic, Brass, long-chipping, Bronze, long-chipping, Copper, low-alloyed |
| Cutting values | |||||||||||||
| For M3-M5 | |||||||||||||
| Material designation | Tensile strength | Machining | M3 | M4 | M5 | ||||||||
| vc | n | f | n | f | n | f | |||||||
| from | to | from | to | from | to | from | to | ||||||
| Steels | |||||||||||||
| General structural steels | ≤ 850 N/mm² | Threads | 5 | 7 | 530 | 743 | 0,50 | 398 | 557 | 0,70 | 318 | 445 | 0,80 |
| Drills | 15 | 23 | 1592 | 2441 | 0,015 | 1194 | 1831 | 0,017 | 955 | 1464 | 0,02 | ||
| Unalloyed quenched and tempered steels | ≤ 850 N/mm² | Threads | 5 | 7 | 530 | 743 | 0,50 | 398 | 557 | 0,70 | 318 | 445 | 0,80 |
| Drills | 15 | 23 | 1592 | 2441 | 0,015 | 1194 | 1831 | 0,017 | 955 | 1464 | 0,02 | ||
| ≤ 1,000 N/mm² | Threads | 3 | 5 | 318 | 530 | 0,50 | 238 | 398 | 0,70 | 191 | 318 | 0,80 | |
| Drills | 12 | 20 | 1273 | 2123 | 0,012 | 955 | 1592 | 0,015 | 764 | 1273 | 0,017 | ||
| Low-alloy quenched and tempered steels | ≤ 850 N/mm² | Threads | 5 | 7 | 530 | 743 | 0,50 | 398 | 557 | 0,70 | 318 | 445 | 0,80 |
| Drills | 15 | 23 | 1592 | 2441 | 0,015 | 1194 | 1831 | 0,017 | 955 | 1464 | 0,02 | ||
| ≤ 1,000 N/mm² | Threads | 3 | 5 | 318 | 530 | 0,50 | 238 | 398 | 0,70 | 191 | 318 | 0,80 | |
| Drills | 12 | 20 | 1273 | 2123 | 0,012 | 955 | 1592 | 0,015 | 764 | 1273 | 0,017 | ||
| Alloyed quenched and tempered steels | ≤ 1,200 N/mm² | Threads | 2 | 3 | 212 | 318 | 0,50 | 159 | 238 | 0,70 | 127 | 191 | 0,80 |
| Drills | 8 | 13 | 849 | 1380 | 0,012 | 636 | 1035 | 0,015 | 509 | 828 | 0,017 | ||
| Nitriding steels | ≤ 1,200 N/mm² | Threads | 2 | 3 | 212 | 318 | 0,50 | 159 | 238 | 0,70 | 127 | 191 | 0,80 |
| Drills | 8 | 13 | 849 | 1380 | 0,012 | 636 | 1035 | 0,015 | 509 | 828 | 0,017 | ||
| Tool steels | ≤ 1,200 N/mm² | Threads | 2 | 3 | 212 | 318 | 0,50 | 159 | 238 | 0,70 | 127 | 191 | 0,80 |
| Drills | 8 | 13 | 849 | 1380 | 0,012 | 636 | 1035 | 0,015 | 509 | 828 | 0,017 | ||
| High-speed steels | ≤ 1,200 N/mm² | Threads | 2 | 3 | 212 | 318 | 0,50 | 159 | 238 | 0,70 | 127 | 191 | 0,80 |
| Drills | 8 | 13 | 849 | 1380 | 0,012 | 636 | 1035 | 0,015 | 509 | 828 | 0,017 | ||
| Stainless steels | |||||||||||||
| Stainless steels | ≤ 1,200 N/mm² | Threads | 1,5 | 2 | 159 | 212 | 0,50 | 119 | 159 | 0,70 | 95 | 127 | 0,80 |
| Drills | 6 | 9 | 636 | 955 | 0,012 | 477 | 716 | 0,014 | 382 | 573 | 0,016 | ||
| Titanium and titanium alloys | ≤ 850 N/mm² | Threads | 0,8 | 1,5 | 84 | 159 | 0,50 | 63 | 119 | 0,70 | 50 | 95 | 0,80 |
| Drills | 3 | 5 | 318 | 530 | 0,015 | 238 | 398 | 0,017 | 191 | 318 | 0,019 | ||
| Special alloys | ≤ 1,200 N/mm² | Threads | 0,7 | 1,3 | 74 | 138 | 0,50 | 55 | 103 | 0,70 | 44 | 82 | 0,80 |
| Drills | 2 | 4 | 212 | 424 | 0,015 | 159 | 318 | 0,017 | 127 | 254 | 0,019 | ||
| Cast metals | |||||||||||||
| Cast iron | ≤ 300 HB | Threads | 5 | 7 | 530 | 743 | 0,50 | 398 | 557 | 0,70 | 318 | 445 | 0,80 |
| Drills | 12 | 20 | 1273 | 2123 | 0,012 | 955 | 1592 | 0,015 | 764 | 1273 | 0,017 | ||
| Spheroidal graphite and malleable iron | ≤ 350 HB | Threads | 3 | 5 | 318 | 530 | 0,50 | 238 | 398 | 0,70 | 191 | 318 | 0,80 |
| Drills | 10 | 16 | 1061 | 1698 | 0,012 | 796 | 1273 | 0,015 | 636 | 1019 | 0,017 | ||
| Non-ferrous metals | |||||||||||||
| Aluminium | ≤ 450 N/mm² | Threads | 7 | 9 | 743 | 955 | 0,50 | 557 | 716 | 0,70 | 445 | 573 | 0,80 |
| Drills | 18 | 25 | 1910 | 2653 | 0,015 | 1433 | 1990 | 0,017 | 1146 | 1592 | 0,02 | ||
| Aluminium alloys | ≤ 450 N/mm² | Threads | 6 | 8 | 636 | 849 | 0,50 | 477 | 636 | 0,70 | 382 | 509 | 0,80 |
| Drills | 16 | 23 | 1698 | 2441 | 0,015 | 1273 | 1831 | 0,017 | 1019 | 1464 | 0,02 | ||
| Wrought aluminium alloys | ≤ 400 N/mm² | Threads | 6 | 8 | 636 | 849 | 0,50 | 477 | 636 | 0,70 | 382 | 509 | 0,80 |
| Drills | 16 | 23 | 1698 | 2441 | 0,015 | 1273 | 1831 | 0,017 | 1019 | 1464 | 0,02 | ||
| Cast aluminium alloys ≤ 10% Si | ≤ 600 N/mm² | Threads | 5 | 7 | 530 | 743 | 0,50 | 398 | 557 | 0,70 | 318 | 445 | 0,80 |
| Drills | 15 | 23 | 1592 | 2441 | 0,015 | 1194 | 1831 | 0,017 | 955 | 1464 | 0,02 | ||
| Low-alloy copper | ≤ 400 N/mm² | Threads | 7 | 9 | 743 | 955 | 0,50 | 557 | 716 | 0,70 | 445 | 573 | 0,80 |
| Drills | 18 | 25 | 1910 | 2653 | 0,015 | 1433 | 1990 | 0,017 | 1146 | 1592 | 0,02 | ||
| Long-chipping brass | ≤ 600 N/mm² | Threads | 6 | 8 | 636 | 849 | 0,50 | 477 | 636 | 0,70 | 382 | 509 | 0,80 |
| Drills | 17 | 23 | 1800 | 2440 | 0,015 | 1353 | 1831 | 0,017 | 1082 | 1464 | 0,02 | ||
| Bronze, long-chipping | ≤ 850 N/mm² | Threads | 4 | 6 | 424 | 636 | 0,50 | 318 | 477 | 0,70 | 254 | 382 | 0,80 |
| Drills | 15 | 21 | 1592 | 2229 | 0,012 | 1194 | 1671 | 0,015 | 955 | 1337 | 0,017 | ||
| Plastics | |||||||||||||
| Plastics, thermosetting | Threads | 7 | 9 | 743 | 955 | 0,50 | 557 | 716 | 0,70 | 445 | 573 | 0,80 | |
| Drills | 18 | 27 | 1910 | 2866 | 0,015 | 1433 | 2149 | 0,017 | 1146 | 1719 | 0,02 | ||
| Plastics, thermoplastic | Threads | 7 | 9 | 743 | 955 | 0,50 | 557 | 716 | 0,70 | 445 | 573 | 0,80 | |
| Drills | 18 | 26 | 1910 | 2760 | 0,015 | 1433 | 2070 | 0,017 | 1146 | 1656 | 0,02 | ||
| Key |
| vc = cutting speed [m/min] |
| f = feed [mm/r] |
| n = rotation speed [rpm] |
| The suggested cutting values are reference values and must be adapted to the respective conditions. |
| Cutting values | |||||||||||||
| For M6-M10 | |||||||||||||
| Material designation | Tensile strength | Machining | M6 | M8 | M10 | ||||||||
| vc | n | f | n | f | n | f | |||||||
| from | to | from | to | from | to | from | to | ||||||
| Steels | |||||||||||||
| General structural steels | ≤ 850 N/mm² | Threads | 5 | 7 | 265 | 371 | 1,00 | 199 | 278 | 1,25 | 159 | 222 | 1,50 |
| Drills | 15 | 23 | 796 | 1220 | 0,022 | 597 | 915 | 0,025 | 477 | 732 | 0,027 | ||
| Unalloyed quenched and tempered steels | ≤ 850 N/mm² | Threads | 5 | 7 | 265 | 371 | 1,00 | 199 | 278 | 1,25 | 159 | 222 | 1,50 |
| Drills | 15 | 23 | 796 | 1220 | 0,022 | 597 | 915 | 0,025 | 477 | 732 | 0,027 | ||
| ≤ 1,000 N/mm² | Threads | 3 | 5 | 159 | 265 | 1,00 | 119 | 199 | 1,25 | 95 | 159 | 1,50 | |
| Drills | 12 | 20 | 636 | 1061 | 0,019 | 477 | 796 | 0,022 | 382 | 636 | 0,025 | ||
| Low-alloy quenched and tempered steels | ≤ 850 N/mm² | Threads | 5 | 7 | 265 | 371 | 1,00 | 199 | 278 | 1,25 | 159 | 222 | 1,50 |
| Drills | 15 | 23 | 796 | 1220 | 0,022 | 597 | 915 | 0,025 | 477 | 732 | 0,027 | ||
| ≤ 1,000 N/mm² | Threads | 3 | 5 | 159 | 265 | 1,00 | 119 | 199 | 1,25 | 95 | 159 | 1,50 | |
| Drills | 12 | 20 | 636 | 1061 | 0,019 | 477 | 796 | 0,022 | 382 | 636 | 0,025 | ||
| Alloyed quenched and tempered steels | ≤ 1,200 N/mm² | Threads | 2 | 3 | 106 | 159 | 1,00 | 79 | 119 | 1,25 | 63 | 95 | 1,50 |
| Drills | 8 | 13 | 424 | 690 | 0,019 | 318 | 517 | 0,022 | 254 | 414 | 0,025 | ||
| Nitriding steels | ≤ 1,200 N/mm² | Threads | 2 | 3 | 106 | 159 | 1,00 | 79 | 119 | 1,25 | 63 | 95 | 1,50 |
| Drills | 8 | 13 | 424 | 690 | 0,019 | 318 | 517 | 0,022 | 254 | 414 | 0,025 | ||
| Tool steels | ≤ 1,200 N/mm² | Threads | 2 | 3 | 106 | 159 | 1,00 | 79 | 119 | 1,25 | 63 | 95 | 1,50 |
| Drills | 8 | 13 | 424 | 690 | 0,019 | 318 | 517 | 0,022 | 254 | 414 | 0,025 | ||
| High-speed steels | ≤ 1,200 N/mm² | Threads | 2 | 3 | 106 | 159 | 1,00 | 79 | 119 | 1,25 | 63 | 95 | 1,50 |
| Drills | 8 | 13 | 424 | 690 | 0,019 | 318 | 517 | 0,022 | 254 | 414 | 0,025 | ||
| Stainless steels | |||||||||||||
| Stainless steels | ≤ 1,200 N/mm² | Threads | 1,5 | 2 | 79 | 106 | 1,00 | 59 | 79 | 1,25 | 48 | 63 | 1,50 |
| Drills | 6 | 9 | 318 | 477 | 0,02 | 238 | 358 | 0,25 | 191 | 286 | 0,027 | ||
| Titanium and titanium alloys | ≤ 850 N/mm² | Threads | 0,8 | 1,5 | 42 | 79 | 1,00 | 31 | 59 | 1,25 | 25 | 47 | 1,50 |
| Drills | 3 | 5 | 159 | 265 | 0,021 | 119 | 199 | 0,023 | 95 | 159 | 0,025 | ||
| Special alloys | ≤ 1,200 N/mm² | Threads | 0,7 | 1,3 | 37 | 69 | 1,00 | 27 | 51 | 1,25 | 22 | 41 | 1,50 |
| Drills | 2 | 4 | 106 | 212 | 0,021 | 79 | 159 | 0,023 | 63 | 127 | 0,025 | ||
| Cast metals | |||||||||||||
| Cast iron | ≤ 300 HB | Threads | 5 | 7 | 265 | 371 | 1,00 | 199 | 278 | 1,25 | 159 | 222 | 1,50 |
| Drills | 12 | 20 | 636 | 1061 | 0,019 | 477 | 796 | 0,022 | 382 | 636 | 0,025 | ||
| Spheroidal graphite and malleable iron | ≤ 350 HB | Threads | 3 | 5 | 159 | 265 | 1,00 | 119 | 199 | 1,25 | 95 | 159 | 1,50 |
| Drills | 10 | 16 | 530 | 849 | 0,019 | 398 | 636 | 0,022 | 318 | 509 | 0,025 | ||
| Non-ferrous metals | |||||||||||||
| Aluminium | ≤ 450 N/mm² | Threads | 7 | 9 | 371 | 477 | 1,00 | 278 | 358 | 1,25 | 222 | 286 | 1,50 |
| Drills | 18 | 25 | 955 | 1326 | 0,022 | 716 | 995 | 0,025 | 573 | 796 | 0,027 | ||
| Aluminium alloys | ≤ 450 N/mm² | Threads | 6 | 8 | 318 | 424 | 1,00 | 238 | 318 | 1,25 | 191 | 254 | 1,50 |
| Drills | 16 | 23 | 849 | 1220 | 0,022 | 636 | 915 | 0,025 | 509 | 732 | 0,027 | ||
| Wrought aluminium alloys | ≤ 400 N/mm² | Threads | 6 | 8 | 318 | 424 | 1,00 | 238 | 318 | 1,25 | 191 | 254 | 1,50 |
| Drills | 16 | 23 | 849 | 1220 | 0,022 | 636 | 915 | 0,025 | 509 | 732 | 0,027 | ||
| Cast aluminium alloys ≤ 10% Si | ≤ 600 N/mm² | Threads | 5 | 7 | 265 | 371 | 1,00 | 199 | 278 | 1,25 | 159 | 222 | 1,50 |
| Drills | 15 | 23 | 796 | 1220 | 0,022 | 597 | 915 | 0,025 | 477 | 732 | 0,027 | ||
| Low-alloy copper | ≤ 400 N/mm² | Threads | 7 | 9 | 371 | 477 | 1,00 | 278 | 358 | 1,25 | 222 | 286 | 1,50 |
| Drills | 18 | 25 | 955 | 1326 | 0,022 | 716 | 995 | 0,025 | 573 | 796 | 0,027 | ||
| Long-chipping brass | ≤ 600 N/mm² | Threads | 6 | 8 | 318 | 424 | 1,00 | 238 | 318 | 1,25 | 191 | 254 | 1,50 |
| Drills | 17 | 23 | 902 | 1220 | 0,022 | 676 | 915 | 0,025 | 541 | 732 | 0,027 | ||
| Bronze, long-chipping | ≤ 850 N/mm² | Threads | 4 | 6 | 212 | 318 | 1,00 | 159 | 238 | 1,25 | 127 | 191 | 1,50 |
| Drills | 15 | 21 | 796 | 1114 | 0,019 | 597 | 835 | 0,022 | 477 | 668 | 0,025 | ||
| Plastics | |||||||||||||
| Plastics, thermosetting | Threads | 7 | 9 | 371 | 477 | 1,00 | 278 | 358 | 1,25 | 222 | 286 | 1,50 | |
| Drills | 18 | 27 | 955 | 1433 | 0,022 | 716 | 1074 | 0,025 | 573 | 859 | 0,027 | ||
| Plastics, thermoplastic | Threads | 7 | 9 | 371 | 477 | 1,00 | 278 | 358 | 1,25 | 222 | 286 | 1,50 | |
| Drills | 18 | 26 | 955 | 1380 | 0,022 | 716 | 1035 | 0,025 | 573 | 828 | 0,027 | ||
Just leave the field empty if you don't know the packaging unit when directly entering the article number in the shopping basket or when importing with v
VVVV = 4 digits for prefix number (please note that the first digit is currently always 0)
AAA = 3 digits for dimension part 1
BBB = 3 digits for dimension part 2
Example article number structures:
Example 1: Screw with dimensions of 4x10 mm:
VVVVAAABBB
00574 10 (2 spaces between the 4 and the 10)
Example 2: Screw with dimensions of 10x20 mm:
VVVVAAABBB
005710 20 (1 space between the 10 and the 20)
Example 3: Flat washer with an internal diameter of 6 mm:
VVVVAAABBB
04076
The displayed price is always in line with the displayed packaging, if the PU is 250 the price for 250 units, if the PU is 300 the price for 300 units.
Price with price key representation (PSL):
The price always applies to a quantity ruled through the price key:
Price for 1 unit
Price for 100 units
Price for 1000 units
Select RAL-colour code
!! NOTE: On-screen visualisation of the colour differs from real colour shade!!
Last viewed

SMART STEP EU+ HSCo nanoProtect hexagon combination screw tap assortment 6 pieces

1/2 inch impact socket wrench insert, extra long set 3 pieces

Flat blunt-ended file DIN 7261, shape A

Nylon Sanding Fleece suitable for manual and machine use

Release tool for connectors with multiple locking lugs

Blind rivet, flat head
Blind rivet, flat head

1/2 inch impact socket wrench set inch hexagon Short, 11 pieces

SMART STEP EU+ HSCo nanoProtect hexagon twist drill bit for drill/drivers and tangential impact drivers

1/2-inch impact socket wrench assortment 12 pieces