


Solid carbide end mill Speedcut, ultra-hard steel 68 HRC, corner radius long, optional
ENDMIL-SP-DIN6527L-HS-SC-HA-D16X0,5
Art.-no. 5443300905
EAN 4055375894354


Register now and access more than 125,000 products
Datasheets(X)

 | |
Product code | 6647 |
Material to be processed | Cast metal, Hard and tough material |
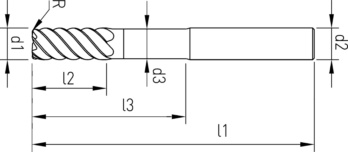
Diameter (d1) | 16 mm |
Shank diameter (d2) | 16 mm |
Clearance diameter (d3) | 15.8 mm |
Standards | CS |
Construction length | Long |
Shank style | Cylindrical DIN 6535-HA |
Cutting material | SC |
Surface | TiAlN-S |
Coolant supply | External |
Twist angle | 50° |
Corner radius (R) | 0.5 mm |
Length (l1) | 92 mm |
Cutting edge length (l2) | 25 mm |
Clearance length (l3) | 38 mm |
Number of cutting edges (Z) | 8 PCS |
Tolerance of cutting edge diameter | e8 |
Tolerance of shank diameter | h5 |
Material of sub-group | Alloyed tempering steels < 1000 N/mm², Nitriding steels < 1300 N/mm², Grey cast iron, Malleable cast iron, Steels > 45 HRC |
| Cutting values finishing contour | ||||||||||
| For dia. 4 - dia. 16 | ||||||||||
| Material designation | Tensile strength | Cooling | vc | fz | ||||||
| Dia. 4 | Dia. 5 | Dia. 6 | Dia. 8 | Dia. 10 | Dia. 12 | Dia. 16 | ||||
| Tool steels | 1100–1400 N/mm2 | T | 170 | 0,010 | 0,015 | 0,020 | 0,025 | 0,030 | 0,035 | 0,040 |
| Hardened steels | 40–48 HRC | T | 150 | 0,010 | 0,015 | 0,020 | 0,030 | 0,035 | 0,040 | 0,050 |
| 48–55 HRC | T | 135 | 0,010 | 0,015 | 0,020 | 0,025 | 0,030 | 0,035 | 0,045 | |
| 55–60 HRC | T | 120 | 0,008 | 0,012 | 0,015 | 0,025 | 0,030 | 0,035 | 0,045 | |
| 60–68 HRC | T | 80 | 0,008 | 0,012 | 0,015 | 0,020 | 0,025 | 0,030 | 0,035 | |
| Wear resistant constructional steel | 1350 N/mm2 | T | 170 | 0,010 | 0,015 | 0,020 | 0,025 | 0,025 | 0,035 | 0,040 |
| 1800 N/mm2 | T | 145 | 0,010 | 0,015 | 0,020 | 0,025 | 0,025 | 0,035 | 0,040 | |
| Cast iron | < 180 HB | T | 200 | 0,015 | 0,022 | 0,030 | 0,040 | 0,055 | 0,065 | 0,080 |
| > 180 HB | T | 160 | 0,015 | 0,022 | 0,030 | 0,040 | 0,050 | 0,060 | 0,070 | |
| Spheroidal graphite, malleable iron | > 180 HB | T | 190 | 0,015 | 0,022 | 0,030 | 0,040 | 0,055 | 0,065 | 0,080 |
| > 260 HB | T | 170 | 0,015 | 0,022 | 0,030 | 0,040 | 0,050 | 0,060 | 0,070 | |
| Legend | ||
| T = dry | 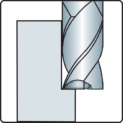 | ae = 0.02xd1 |
| vc = cutting speed [m/min] | ||
| fz = feed per tooth [mm/z] | ap = 1.5xd1 | |
| ae = cutting thickness (radial) | ||
| ap = cutting thickness (axial) | ||
| The cutting speeds listed refer to all tool types according to DIN 6527K or DIN6527L. For XL Series end mills, it is recommended to reduce the cutting speed by 30%. | ||
Last viewed

Spring band clamp pliers, large

HDPE UV fold masker

Slotted cheese head DIN 84, A2 stainless steel, plain

HDPE fold masker

Male thread safety coupling Series 2000

WÜRTH MODYF Fornax S3L welder's safety boot
Hexagon nut with flange EN 1661, steel 10, zinc-nickel-plated, silver (ZNSHL)

Countersunk tapping screw type C with H recessed head ISO 7050, A2 stainless steel, plain

Series 4000 plug-in nipple with female thread

3/4-inch impact socket wrench insert hexagon, metric, short